
Filter by Form
- SS 310 and 310S: High-Temperature Grades
- 904L Stainless Steel: Sheet, Pipe, Bar and Coil [CO:wp/v2/products/name]
- Plate & Sheet Supplier [CO:wp/v2/products/name]
- Tube & Pipe
- Bar & Rod
- Coils & Coil Stock
- Profiles
Filter by Grade Family
- Austenitic Grades
- Duplex Grades
- Ferritic Grades
- Martensitic Grades
- Precipitation Hardening Grades
Filter by Rolling Condition
- Cold Rolled
- Hot Rolled
-
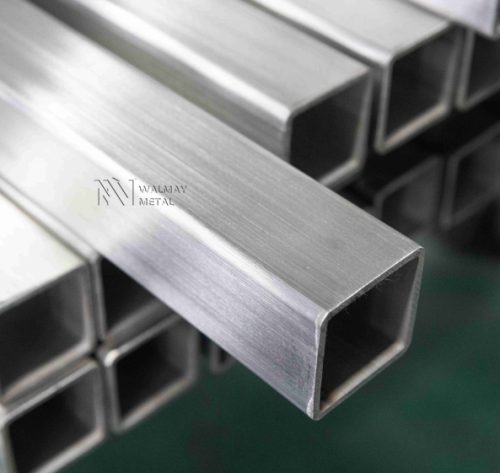 Pipe / Tube Stainless Steel Rectangular Tube
-
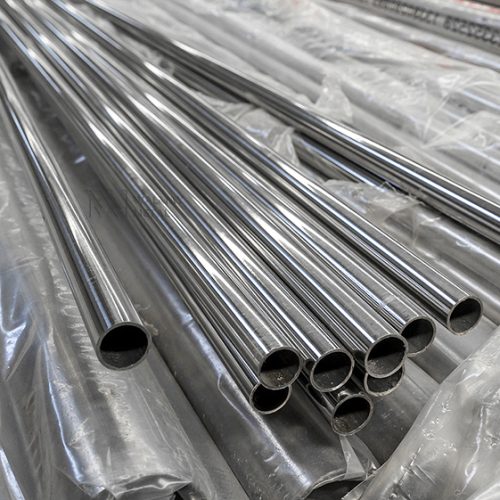 Pipe / Tube Seamless Stainless Steel Pipe [CO:wp/v2/product/title]Industrial stainless steel product. [CO:wp/v2/product/excerpt]
-
Pipe / Tube 304 Stainless Steel Pipe and Tube
-
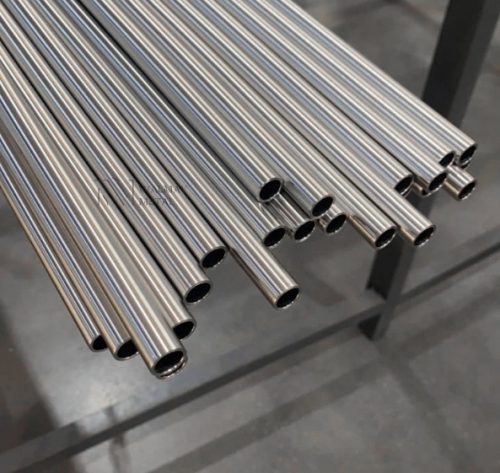 Pipe / Tube 304L Stainless Steel PipeUltra-Low Carbon Food-Grade Pipe, Ensures Weld Purity for Dairy, Brewery, and High-Purity Water Conveyance Systems
-
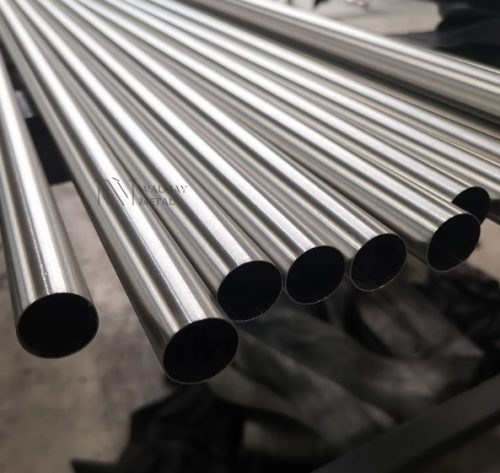 Pipe / Tube 316 Stainless Steel Pipe and Tube
-
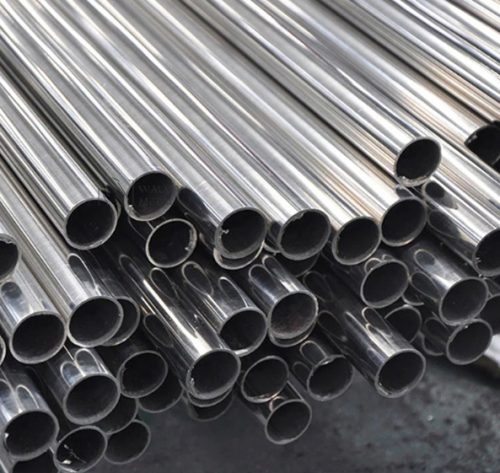 Pipe / Tube 430 stainless steel pipeOD 20–63mm | Excellent Formability & Corrosion Resistance | Ideal for Home Appliances, Kitchenware & Decorative Structur
-
 Pipe / Tube 321 Stainless Steel Tubing and Seamless Pipe
-
 Pipe / Tube Duplex 2205 Pipe
-
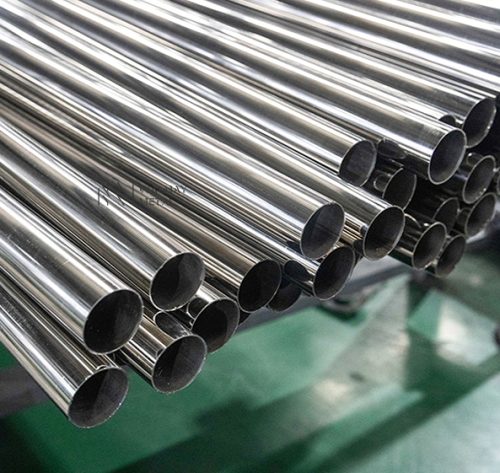 310 / 310S 310 Stainless Steel Pipe and 310S Tube
-
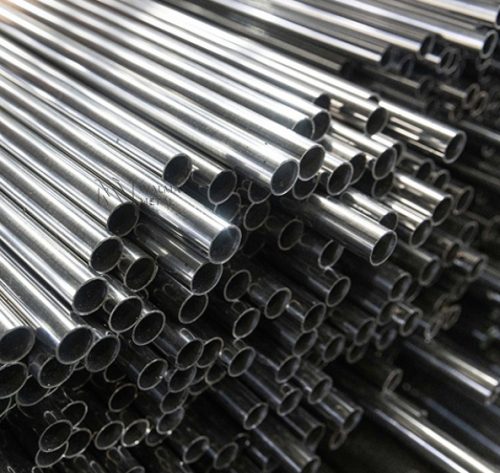 Pipe / Tube 316L Stainless Steel Pipe
-
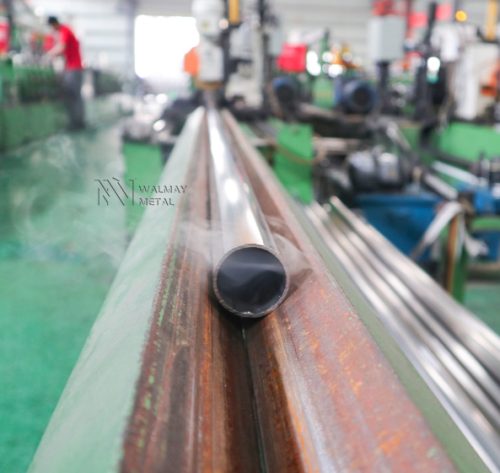 Pipe / Tube 410 Stainless Steel PipeNeed custom quenching specifications or cut-to-length services? Message our engineers on email for a fast technical quot
-
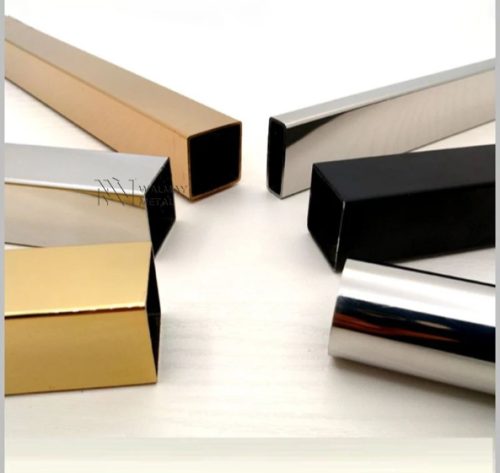 Pipe / Tube 201 Decorative Welded Steel PipeDesigned for hotel handrails, commercial display stands, furniture frames, and architectural trim structures across Euro